


Medicine Pillow Bag
Our medicine pillow bags deliver reliable sterility and safety protection for pharmaceuticals and medical devices. Manufactured with medical‑grade multi‑layer composite films including plastic and aluminium foil, our packaging creates an effective sterile barrier while remaining non‑toxic and odour‑free. We provide flexible customisation over size, shape and capacity to suit varied‑dose medicines and special‑shaped medical instruments. Custom‑printed colours, patterns and logos help strengthen your brand recognition and market competitiveness.
Smart traceability solutions such as QR codes, anti‑counterfeit ink and laser holographic labels enable full‑lifecycle product monitoring for batch information checking, anti‑counterfeiting and anti‑diversion management. Degradable options made from PLA and biodegradable plastics are also available, meeting strict pharmaceutical packaging specifications while lowering environmental pollution.
Product Features
Our Cases
Professional Roll‑film Solutions for Pharmaceutical Pillow‑Bag Packaging
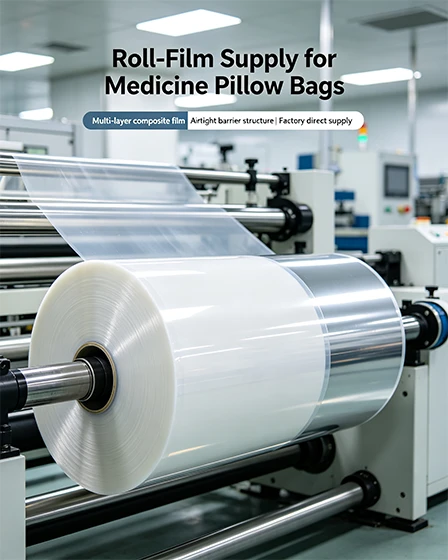
Roll‑film for Medicine Pillow Bags
We supply finished multi‑layer composite roll‑film for automatic pillow‑bag packaging machines.
This aluminum‑plastic barrier film is specially developed for capsule, tablet and medical‑consumable packaging.
Our roll‑film meets pharmaceutical‑grade safety standards, delivering excellent protection against oxygen, moisture and light to keep your drugs stable during their shelf‑life.
High‑definition custom printing, QR‑code traceability and anti‑counterfeiting functions can be finished on the roll‑film before delivery.
You can run the film directly on your existing pillow‑packing production line, saving extra pouch‑making costs and improving your packing efficiency.
Medical‑Grade Film Structure
Our multi‑layer composite roll‑film is engineered specifically for pharmaceutical pillow‑bag packaging.
It integrates excellent oxygen‑barrier, moisture‑resistant and light‑shielding performance.
The chemically‑inert material contains no harmful substances, with zero risk of chemical reaction with medicines.
Each layer is strictly produced under clean‑room standards, creating a reliable sterile barrier to protect capsules, tablets and medical supplies throughout shelf‑life.
We customize film thickness and composite structure to match your specific pharmaceutical storage requirements.


Printed & Traceable Before Delivery
We can integrate QR codes, serial numbers, laser anti-counterfeiting marks and security ink directly onto the film. This enables full-cycle product traceability, anti-diversion control and counterfeit prevention, helping you stay fully compliant with pharmaceutical industry supervision requirements.
Full‑customizable Roll‑film & One‑stop Solution
We provide flexible customization for roll‑film width, thickness, multi‑layer composite structure and printing designs. Various specifications can be tailored to fit tablets, capsules and small‑size medical‑consumable pillow‑packaging requirements.
All our pharmaceutical roll‑films are well compatible with most automatic pillow‑bag packaging machines. Clients can use the delivered roll‑film directly on‑site, cutting extra pouch‑making procedures, lowering production costs and improving your packaging efficiency.

Application Scenarios
Our pharmaceutical‑grade roll‑film delivers reliable barrier protection for various automatic pillow‑packaging lines. It is widely used for tablets, capsules, medical consumables and granular healthcare products, helping you achieve safe, traceable and high‑efficiency packaging.


Strong Manufacturing Capacity & Full‑line Workshops

Blown‑film Workshop
Equipped with high‑end multi‑layer co‑extrusion lines, our specialized blown‑film workshop independently manufactures mono‑PE barrier films.
Every roll features uniform thickness and exceptional moisture‑oxygen protection.
Continuous strict in‑line quality monitoring throughout the whole production cycle provides rock‑solid quality support for your finished flexible pouches.
Printing Workshop
Our printing workshop houses 8 high‑speed gravure‑printing units.
With premium‑grade printing equipment, we reproduce your brand graphics and logos in high definition with precise colour matching.
The entire printing zone operates under rigorous dust‑control protocols to minimise printing defects, delivering top‑quality printed rolls for downstream conversion processes.


Lamination Workshop
We own a total of 12 high‑speed laminators, including 4 solvent‑free laminators and 8 dry laminators. Located inside our 100,000‑class dust‑free purification workshop, all composite production is carried out under controlled‑environment conditions. Precise parameter monitoring ensures bubble‑free, firmly‑bonded composite films that fully comply with international food‑contact safety standards.
Pouch‑Making Workshop
Our fully‑automatic pouch‑making production lines can manufacture a wide variety of packages, including flat‑bottom pouches, eight‑side‑sealed bags and special‑shaped cat‑ear top pouches.
Precision heat‑sealing technology delivers firm, leak‑proof sealed edges.
Each finished pouch undergoes strict quality inspection prior to shipment, supplying dependable flexible packaging solutions for worldwide pet‑food brands.


One‑Stop Flexible Packaging Manufacturer From China
Send your inquiry about custom flexible packaging solutions to us.
We provide high‑quality food‑grade pouch packaging for pet food, cosmetics, daily‑care and food brands worldwide.
With our FDA, BRC and FSSC22000 certified packaging, you can elevate your products, captivate your customers, and unlock new opportunities for growth and success for your brand.


FAQ
Q: What is your daily production capacity?
A: We have a large-scale production base with over 500 employees, capable of producing 40 million bags per day, plus 50 tons of roll film. This ensures stable supply even for large-volume orders.
Q: What quality tests do you perform?
A: We conduct rigorous in-house tests including puncture resistance, leak testing, seal strength evaluation, and barrier performance checks. Test reports can be provided upon request.
Q: How are the bags packed for shipment?
A: Finished bags are packed in sturdy export cartons, with quantities per carton customizable based on bag size and customer preference to optimize shipping and storage.
Q: How long has Secia Pack been in the packaging industry?
A: Secia Pack was established in 2006, with 20 years of experience specializing in aluminum foil-plastic pouches and roll stocks. We have a 20-member R&D team and an in-house high-level purification lab.
Q: Do you offer eco-friendly / recyclable options?
A: Yes. We provide fully recyclable mono-material structures for brands pursuing sustainability. These options reduce environmental impact while maintaining the required barrier and durability performance.
Hot Tags: Medicine Pillow Bag, China Medicine Pillow Bag manufacturers, suppliers, factory, Testing Reagent Bag, health care, Capsule And Pill Packaging, Medcine Blister


